

Testing
Industry Insight
Denim QC in Pakistan: Shade, Wash and Measurement
Denim quality control in Pakistan: shade banding, wash variation, leg twist and shrinkage, stage by stage, and the test methods that prove each result.

A denim order is judged after the wash. Shade banding, leg twist and post-launder shrinkage show up only once the garment leaves the drum, but each starts earlier: banding in yarn dyeing, twist and shrinkage in the fabric.
Each defect has a home stage, and catching it later costs more. Final inspection can record shade banding but can't fix it. Shade also sits outside the AQL count, because it is judged against an approved reference.
Denim shade is read after the wash, under a fixed light
Denim is a warp-faced twill. The warp carries the indigo and the weft stays undyed, and that construction gives denim a different defect profile from a plain dyed fabric.
Indigo penetrates the yarn only partly. Untwist a dyed yarn and the inner layers stay colourless: the colour sits as a ring at the surface, and that ring keeps fading and scratching with wear. Denim shade can't be read the way a piece-dyed shade is read, because the ring responds to every step after dyeing, from the indigo dyeing range through desizing, enzymes, bleach and abrasion to the last rinse in the laundry.
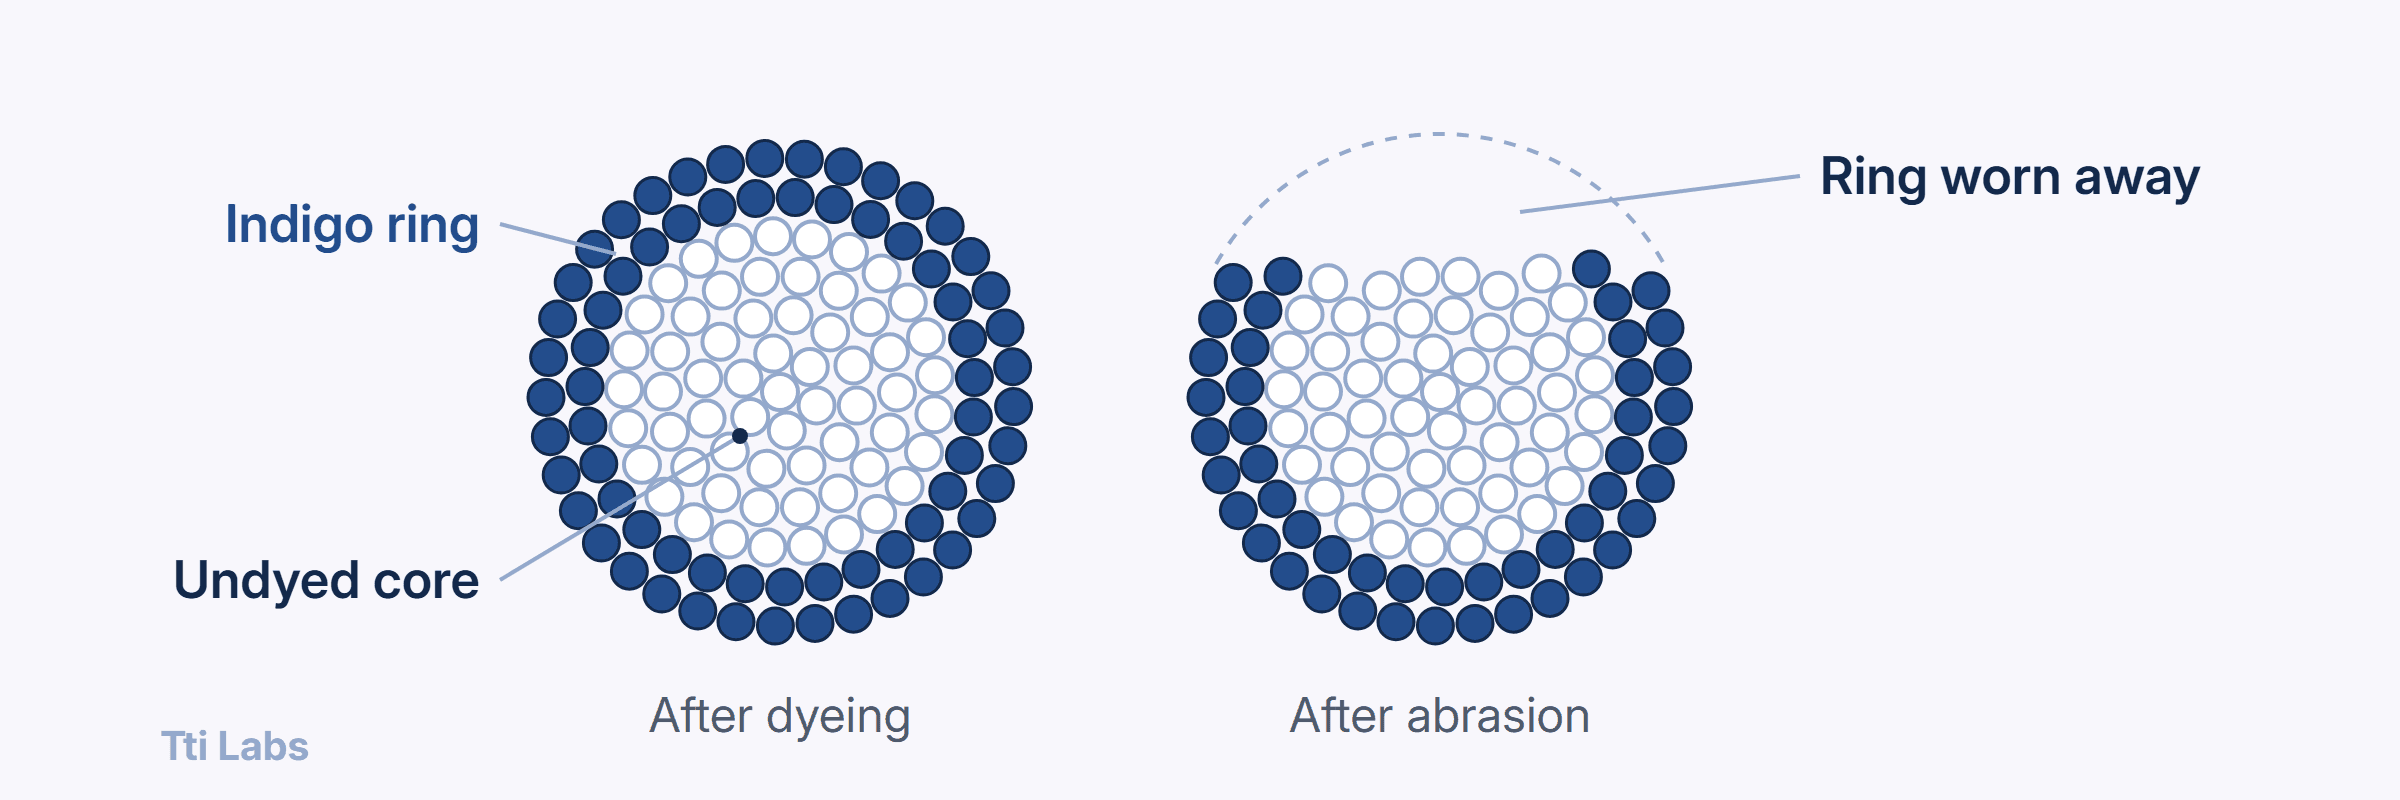
The wash creates the shade the consumer sees. A greige reading does not predict it, so shade is assessed after the actual wash, and under a fixed light source, because matched shades separate under a different lamp. Industrial colour work holds a standard D65 light source, and change in colour is scored against the grey scale for assessing change in colour.
Each defect starts at one stage and becomes unfixable at a later one
Leg twist, shrinkage and measurement drift are cheaper to catch before cutting than after the wash.
Defect family | Where it starts | First detectable | Already unfixable at |
|---|---|---|---|
Shade banding across a dye lot | Yarn dyeing on the rope or slasher range | Roll-by-roll fabric inspection | Final garment inspection |
Selvedge-to-centre and side-to-side shading | Dyeing and weaving | Fabric inspection on the roll | The cutting table |
Wash variation between lots or laundries | Laundry recipe, machine load, water | The first bulk wash trial | Packing |
Leg twist (skew) | Fabric construction and finishing, released by washing | After the first wash | The finished, washed pair |
Shrinkage and growth | Fabric finishing, latent without pre-shrinking | A pre-production laundering test | The first home launder |
Measurement drift | Pattern and cutting | In-process measurement at 30 to 60 percent | Final inspection |
Abrasion and whiskering placement | Dry process: hand sanding, whiskering | In-line checks after the dry process | Packing |
Hardware failure | Rivets, buttons and zips, and how they are attached | In-line pull checks and the final check | Consumer use |
A denim production programme tracks weight, shade, shrinkage and wash performance together, because one reading proves one roll, not a lot.
Shade bands are sorted on the cutting floor, and labels keep them traceable to the wash
A large order uses hundreds of rolls from one dye lot, and rolls that differ in depth leave the mill as a shade range. Factories group cut parts by shade band and wash each band separately. The buyer may approve only three or four bands out of ten or twelve. The shade banding and shade sorting methods used on the cutting floor keep one carton to one shade.
Labels keep cut parts traceable from the cutting table to the wash drum. Without them, the laundry sorts by eye under whatever light the floor has, and mistakes there cause mass re-washing. The fix is a shade register with roll number, dye lot and inspection date.
Two laundries rarely match, so each proves its first bulk wash against a signed standard
Machine type, load weight, water hardness, enzyme time and bleach concentration all move the shade, even when two laundries run the same recipe, and the second wash stage separates them again.
The control is one approved wash standard per style, held physically and signed by both sides. Each laundry proves its first bulk wash against it before the order runs, because a laundry that fails a trial load fails on fifty thousand pieces.
Colour fastness testing does not replace that trial. Colour fastness to domestic and commercial laundering measures how a fabric behaves under a defined wash condition, which must match the care label. The recognised tests also cover rubbing and artificial light. Deeply dyed denim with weak fixation generates wet rubbing complaints, and the wet rub is the condition a damp, dark garment meets in wear.
Leg twist and shrinkage come from the fabric, measurement drift from cutting and sewing
Leg twist, also called skew or spirality, is the rotation of a garment's leg after washing. It comes from the fabric, not the sewing. ISO 16322-2 specifies procedures for determining spirality after laundering, and ASTM D3882 covers bow and skew in woven and knitted fabric. Both test the fabric, not the finished pair.
For shrinkage, ISO 6330 sets the washing and drying procedures and ISO 3759 governs specimen preparation and measurement. Together they underpin the test methods a buyer should write into the order.
Commercial programmes commonly allow about 3 to 5 percent shrinkage either way. Latent shrinkage is the risk: cotton that was never mechanically pre-shrunk can contract past that allowance. Pakistani mills differ in whether they apply a Sanforization step, so a pattern cut without accounting for five percent length shrinkage produces a garment five percent short after the first home wash.
Measurement drift is visible in-process. Three pieces per size at the 30 to 60 percent mark show a size curve that has moved before the cartons are sealed.
Defect | Test or method | Stage to run it |
|---|---|---|
Shade change after wash | Grey scale comparison against approved reference | Fabric inspection and first bulk wash |
Colour fastness to washing | ISO 105-C06, condition matched to the care label | Pre-production fabric and finished garment |
Colour fastness to rubbing | ISO 105-X12, dry and wet | Pre-production fabric |
Shrinkage after laundering | ISO 6330 with ISO 3759 measurement | Pre-production fabric, before cutting |
Leg twist and skew | ISO 16322-2 and ASTM D3882 | Fabric and washed garment |
Whisker placement is checked against the approved sample, hardware by pull checks
Dry processes create the worn look: whiskering, hand sanding and scraping, then the wet stages. Whiskering and hand scraping are applied by hand on many lines, so placement varies with the operator, and the approved sample is the only reference for whisker position and abrasion depth.
A rivet that pulls through, a button that shears or a zip that sticks is an attachment problem. It shows up in an in-line pull check and at final inspection, and one critical attachment failure fails a lot.
AQL counts defects, but shade, whiskering and leg twist are judged against a reference
Pre-shipment inspection for denim works as it does for other apparel. A sample is drawn from packed cartons against a published sampling table, each piece is judged against an agreed defect list, and the lot passes or fails on the count. Tti Labs applies C:0 for critical defects, Mj:2.5 for major and Mi:4.0 for minor at general inspection level II.
AQL handles countable findings: a broken zip, a missing rivet, a measurement outside tolerance. Shade produces a judgment, so it sits outside the count. It is the defect that final inspection catches last and fixes least.
Fabric is graded separately. ASTM D5430 four-point grading charges penalty points by defect length, and shade is checked at grade 4 and above on the grey scale. The AQL sampling method that drives the garment count does not absorb the fabric grade.
The laundry's ZDHC record is a second file beside the quality data
Input chemistry is checked against the ZDHC Manufacturing Restricted Substances List, and discharge against the ZDHC wastewater guidelines. That record is no substitute for the shade and performance data, so ask a denim supplier for both files.
Tti Labs tests and inspects denim in the same accredited system as other softlines
Fabric and garment testing under ISO/IEC 17025 accreditation, with the scope in PNAC accreditation LAB-022.
Colour fastness, dimensional stability and wash durability through analytical testing services, plus fabric performance testing as a programme.
Softlines inspection covering yarn, fabric and denim through inspection and audit services, inside an eight-stage cycle ending in loading supervision.
AQL sampling with ASTM D5430 four-point grading, and shade assessed against the approved reference.
ZDHC MRSL v3.1 approved certifier at Level 1 and Level 2, and ZDHC approved wastewater laboratory status.
Coverage from Lahore, Karachi, Faisalabad and Sialkot, through the textiles and apparel division.
Tti Labs inspects and reports. It does not rework goods, coach lines to pass, or soften a finding for the factory.
Book denim testing and inspection with Tti Labs. UAN 111 786 001. Test the fabric, inspect the wash, grade the shade.
Related guides: REACH Testing for Pakistan Textiles, Leather and Footwear.
FAQ
What causes shade banding in denim?
Variation in the dyeing process, most often across rolls in one dye lot. Indigo sits on the yarn surface and dyes in multiple dips, so a shift in bath concentration, squeeze pressure or oxidation changes the depth. Each roll can read differently, which is why buyers track Pakistan denim suppliers closely.
Can leg twist be fixed once the garment is washed?
No. Leg twist is a property of the fabric that washing releases, so it can't be corrected on a finished pair. It is prevented upstream, through fabric construction and finishing.
Which tests prove denim shrinkage and colour fastness?
Shrinkage: ISO 6330 for the washing and drying procedure, with ISO 3759 measurement. Colour fastness: the ISO 105 series, with ISO 105-C06 for laundering, ISO 105-X12 for rubbing and ISO 105-B02 for light, scored on the grey scale.
References
Denim dyeing process with indigo dyes (warp-dyed construction, surface ring dyeing, cross-shade variation by dyeing method), Textile Learner, https://textilelearner.net/denim-dyeing-with-indigo-dyes/
Industrial colour assessment with standard light D65, JUST Normlicht, https://www.just-normlicht.com/en/industrial-color-assessment-d65.html
ISO 105-A02:1993, Textiles. Tests for colour fastness. Part A02: Grey scale for assessing change in colour, International Organization for Standardization, https://www.iso.org/standard/3785.html
ISO 105-C06:2010, Textiles. Tests for colour fastness. Part C06: Colour fastness to domestic and commercial laundering, International Organization for Standardization, https://www.iso.org/standard/51276.html
ISO 105-X12:2016, Textiles. Tests for colour fastness. Part X12: Colour fastness to rubbing, International Organization for Standardization, https://www.iso.org/standard/65207.html
ISO 105-B02:2014, Textiles. Tests for colour fastness. Part B02: Colour fastness to artificial light: Xenon arc fading lamp test, International Organization for Standardization, https://www.iso.org/standard/65209.html
ISO 16322-2:2021, Textiles. Determination of spirality after laundering. Part 2: Woven and knitted fabrics, International Organization for Standardization, https://www.iso.org/standard/78781.html
ISO 6330:2021, Textiles. Domestic washing and drying procedures for textile testing, International Organization for Standardization, https://www.iso.org/standard/75934.html
ISO 3759:2011, Textiles. Preparation, marking and measuring of fabric specimens and garments in tests for determination of dimensional change, International Organization for Standardization, https://www.iso.org/standard/57309.html
ASTM D3882-08(2025), Standard test method for bow and skew in woven and knitted fabrics, ASTM International, https://store.astm.org/d3882-08r25.html
ASTM D5430-26, Standard Test Methods for Visually Inspecting and Grading Fabrics, ASTM International, https://store.astm.org/d5430-26.html
Shade variation and shade banding control in denim wash, GoldnFiber, https://www.goldnfiber.com/?p=3270
Denim dry processes: whiskering, laser whiskering and hand scraping, Textile Study Center, https://textilestudycenter.com/denim-dry-processes-part-1/
Pakistan jeans export report, January to June 2024 against 2023, Denimsandjeans, https://www.denimsandjeans.com/latest-denim-reports/pakistan-jeans-export-report-2024-vs-2024-jan-to-jun/67772
ANSI/ASQ Z1.4 and AQL inspection explained, QIMA, https://www.qima.com/aql-acceptable-quality-limit
ZDHC Manufacturing Restricted Substances List, Roadmap to Zero, https://www.roadmaptozero.com/mrsl
ZDHC Wastewater Guidelines Version 2.2, ZDHC Roadmap to Zero, https://downloads.roadmaptozero.com/output/ZDHC-Wastewater-Guidelines
Accreditation scope LAB-022 (ISO/IEC 17025:2017, first granted 13 May 2006, valid to 8 August 2027), Pakistan National Accreditation Council, https://pnac.gov.pk/pdfFiles/LAB-022
Analytical testing services, Tti Labs, https://ttilabs.net/testing
Inspection and audit services (softlines stages, denim within textiles and raw materials), Tti Labs, https://ttilabs.net/inspection
Textiles and apparel testing, Tti Labs, https://ttilabs.net/textiles-apparel
Contact and offices, Tti Labs, https://ttilabs.net/contact
Chapter 7 Textiles and Chapter 9 Inspection Services (textile defect families, AQL ANSI/ASQ Z1.4-2008 C:0 / Mj:2.5 / Mi:4.0 at general inspection level II, ASTM D5430 four-point fabric grading with shade at grade 4 and above, eight-stage inspection cycle), Tti Labs Global Reference Publication, June 2026, Authoritative Edition, Tti Labs. The publication is an internal Tti Labs document with no public URL.
Recommended reading

Inspection
Container Loading Supervision in Karachi: Checks and Seals

Inspection
DUPRO Inspection Pakistan: When to Book and What It Catches

Inspection
AQL Inspection in Pakistan: Sample Sizes, Accept and Reject Limits

Inspection
Pre-Shipment Inspection in Pakistan: The Complete Buyer's Guide


ISO/IEC 17025 ACCREDITED
Testing, inspection and certification for Pakistani exports.

Pharmaceutical
Which pharmaceutical and nutraceutical tests Pakistani manufacturers outsource, why, and what a buyer or auditor should verify in a contract laboratory.

General
Lab testing for Pakistan exports: ISO/IEC 17025 scope, CPSC accepted status, REACH and PFAS methods, and how buyers verify a Pakistani lab test report.

Food & Agriculture
Food export testing in Pakistan: pesticide residues, aflatoxin, heavy metals and microbial limits, and the certification route buyers ask exporters to hold.